How to Choose the Right Agitator for Your Process?
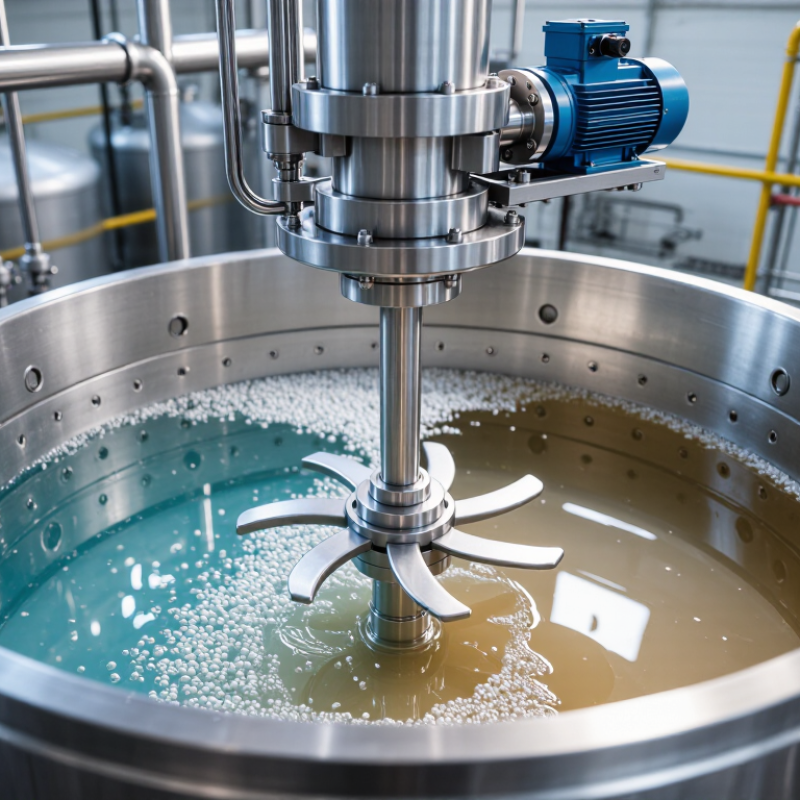
Choosing the right Agitators can determine whether a process runs smoothly or struggles with uneven mixing, wasted energy, and unstable product quality. A suitable design must match the fluid, vessel, operating temperature, solids content, and required mixing result. Water-like liquids may need a different impeller from a viscous polymer or a slurry containing settling particles. Small details matter. A narrow tank, weak motor, or missing baffles can create a strong vortex while leaving dead zones near the bottom.
This guide explains how process engineers evaluate agitator type, impeller diameter, rotational speed, shaft design, and motor power. It also considers shear sensitivity, heat transfer, gas dispersion, and suspension performance. Reliable selection usually combines process calculations, supplier data, operating experience, and pilot testing. Reynolds number and power requirements provide useful direction, but they are not perfect answers. Laboratory results may not fully represent a large production vessel. That limitation deserves attention.
Look closely at the actual process.
A practical assessment should identify what must move, how fast it must move, and what must remain unchanged. Excessive speed may damage fragile particles or introduce air. Insufficient power may allow solids to settle overnight. Experienced suppliers can recommend suitable configurations, yet their advice should be checked against verified process data and maintenance conditions. The best decision balances mixing performance, energy use, cleaning access, equipment reliability, and future production changes. It is not always the most powerful option. Sometimes, a simpler agitator delivers the more dependable result.
Define Process Requirements and Agitation Objectives
How to Choose the Right Agitator for Your Process?
Define process requirements before comparing impeller shapes or motor ratings. Identify viscosity, density, solids concentration, temperature, pressure, and batch volume. Record how these values change during the full cycle. A liquid may begin like water and end like paste.
Then define the agitation objective. Do you need blending, suspension, gas dispersion, heat transfer, or crystallization control? Each goal demands different flow patterns and power input. A high-speed agitator may disperse gas effectively, but it can also create foam, shear-sensitive damage, or unnecessary energy use. The U.S. Department of Energy reports that pumping systems can consume 25% to 50% of industrial facility electricity. Agitator selection deserves the same energy discipline.
Operators should measure mixing time, torque, vessel geometry, and actual batch results. Do not rely only on a catalogue rating. Scale-up is rarely perfect. Small changes in liquid level or solids loading can alter performance. This is where process experience matters, although experience alone can mislead.
Tips: Write the required outcome in measurable terms. For example, “95% concentration uniformity within five minutes” is stronger than “good mixing.” Test the hardest operating condition, not the easiest one. Check startup torque, cleaning needs, seal conditions, and motor efficiency. Keep a record of failed trials. They often reveal the real process requirement.
How to Choose the Right Agitator for Your Process?
Define the process requirements and agitation objectives before selecting an agitator. The chart shows typical screening ranges for power intensity used in common mixing duties; final values depend on viscosity, solids loading, vessel geometry, and scale.
Low-shear blending generally requires modest power input, while gas dispersion and high-solids suspension typically require greater power intensity and stronger circulation. Use these values as an initial design guide, then confirm performance through process calculations or pilot testing.
Match Agitator Design to Fluid Properties
Choosing the right agitator starts with the fluid, not the tank. I have seen efficient equipment fail when viscosity was underestimated. A thin liquid may need a simple axial-flow impeller. A thick paste often requires stronger torque and close-clearance movement. The wrong design can leave stagnant zones near the wall.
Density and solids content also shape the decision. Suspended particles need enough bottom flow to prevent settling. However, excessive speed can damage fragile crystals or create unnecessary heat.
Shear-sensitive products may perform better with gentle, large-diameter blades. Gas-liquid processes need a design that disperses bubbles without flooding. Small details matter here.
Temperature changes can alter viscosity during operation. Corrosive fluids may require careful material selection and seal protection. I recommend checking laboratory data, operating history, and the complete mixing objective together. Power consumption alone is not a reliable selection guide. Torque, flow pattern, shear rate, and cleanability deserve equal attention. A pilot test can reveal behavior that calculations miss. It is not always practical, though. This is where conservative assumptions become useful.
A mistake I still see is choosing an agitator by tank volume alone. Two tanks with equal capacity may need completely different designs. Review the fluid at startup, normal operation, and shutdown. Ask whether the process needs blending, suspension, heat transfer, or gas dispersion. The best match is rarely the fastest one.
Select Impeller Type, Size, and Operating Speed
How to Choose the Right Agitator for Your Process?
Select Impeller Type, Size, and Operating Speed
Choosing an agitator starts with process behavior, not tank volume alone. Examine viscosity, solids concentration, gas dispersion, shear sensitivity, and heat transfer needs. An axial-flow impeller suits blending and suspension in many low-to-medium viscosity liquids. A radial-flow design may provide stronger gas dispersion or localized shear. The wrong type can create dead zones, foaming, or unnecessary power consumption.
Impeller size should match the tank geometry and mixing objective. There is no universal diameter ratio. A larger impeller usually moves more fluid at lower speed, while a smaller one needs higher speed to deliver similar circulation. Check power per volume, torque, tip speed, and motor capacity together. High speed can damage fragile particles or increase vortex formation. In practice, the first estimate is rarely perfect. That matters.
Tips: Compare at least two impeller options using measured process data. Test the most uncertain condition, such as maximum viscosity or solids loading. Watch the liquid surface, motor load, temperature profile, and mixing time. A pilot test can reveal problems calculations miss. Keep records of each trial. Even a simple log improves future scale-up decisions. Ask a qualified mixing engineer to review the final selection, especially when the process changes during operation.
How to Choose the Right Agitator for Your Process? - Select Impeller Type, Size, and Operating Speed
| Process Objective | Recommended Impeller Type | Typical Fluid Viscosity | Typical Impeller-to-Tank Diameter Ratio (D/T) | Typical Operating Speed | Preferred Flow Pattern | Key Selection Notes |
| General liquid blending | 45° pitched-blade turbine | 1–5,000 mPa·s | 0.30–0.50 | 30–150 rpm | Axial with moderate radial circulation | A versatile starting point for low- to medium-viscosity liquids; use multiple impellers in tall tanks. |
| Solid suspension | High-efficiency hydrofoil | 1–2,000 mPa·s | 0.35–0.60 | 60–250 rpm | Strong axial pumping | Select sufficient bottom clearance and power to maintain the required off-bottom solids suspension speed. |
| Gas dispersion | Radial-blade turbine | 1–500 mPa·s | 0.25–0.45 | 100–600 rpm | Radial discharge | Useful when shear and gas breakup are important; check flooding limits and gas flow rate. |
| Gas dispersion with lower shear | Pitched-blade turbine | 1–1,000 mPa·s | 0.30–0.50 | 60–300 rpm | Axial or mixed flow | Provides circulation with less localized shear than a radial turbine in many services. |
| High-viscosity blending | Anchor | 1,000–100,000 mPa·s | 0.85–0.98 | 5–60 rpm | Near-wall circumferential flow | Provides good wall sweeping and heat-transfer performance; maintain adequate clearance to avoid excessive torque. |
| Very high-viscosity or paste mixing | Helical ribbon | 10,000–1,000,000 mPa·s | 0.90–0.98 | 2–40 rpm | Axial and helical circulation | Suitable for laminar mixing; calculate shaft torque carefully and consider a heavy-duty gearbox. |
| Heat-transfer improvement | Anchor with wall scrapers | 1,000–200,000 mPa·s | 0.90–0.98 | 5–50 rpm | Near-wall sweeping | Scrapers reduce stagnant layers and fouling; confirm scraper material compatibility and allowable wall stress. |
| Fast low-viscosity blending | Marine propeller | 1–500 mPa·s | 0.25–0.45 | 100–800 rpm | Strong axial flow | Efficient for rapid turnover and blending when high shear is not the primary requirement. |
| Liquid-liquid dispersion | High-shear rotor-stator or radial turbine | 1–5,000 mPa·s | 0.20–0.50 | 500–3,600 rpm | Localized high-shear circulation | Use when droplet-size reduction is required; control temperature, aeration, and emulsion stability. |
| Gentle blending of shear-sensitive materials | Hydrofoil or large-diameter pitched-blade turbine | 1–2,000 mPa·s | 0.40–0.70 | 20–120 rpm | High-flow, low-shear axial | Favor a larger impeller at lower speed to achieve circulation while limiting shear and heat generation. |
Selection guideline: The ranges above are preliminary design starting points. Final impeller diameter, speed, power, shaft strength, baffle arrangement, liquid level, gas rate, and residence time should be verified using process data, scale-up testing, and mechanical design calculations.
Validate Performance Through Testing and Process Optimization
How to Choose the Right Agitator for Your Process?
Validate performance before approving an agitator for production. A catalog power rating cannot predict real mixing quality. Test the actual liquid, solids loading, temperature, viscosity, and vessel geometry. Measure blend time, power draw, torque, temperature uniformity, and suspended solids. These results reveal whether the selected impeller works under operating conditions.
The International Energy Agency reported that industry consumed about 37% of global final energy in 2022. Even modest mixing improvements can therefore support wider efficiency goals. The U.S. Department of Energy’s Industrial Decarbonization Roadmap also identifies energy efficiency and process optimization as near-term industrial priorities. Use these principles practically.
Compare energy per batch, not only motor efficiency. Check performance at minimum and maximum fill levels. A test at one speed is rarely enough.
Tips:
- Record mixing time with a clear tracer or conductivity change.
- Test startup torque when solids settle overnight.
- Watch for vortexing, splashing, and dead zones.
- Keep one result imperfect. It may expose a hidden operating risk.
- Recheck the vessel after scale-up, because geometric changes can alter circulation patterns.
- Use measured data to refine speed, impeller clearance, and batch sequence.
- Document every adjustment, including failures.
According to the DOE Pumping System Assessment Tool methodology, measured operating data supports more reliable equipment decisions than assumptions alone. The same discipline applies to agitator selection.